QC field copy
The full inspection package for the field inspector, with hold points and a field-change log.
- Logs, line class and NDE requirements
- Walkdowns and test record
- Issued to a named inspector
NODARC welds, fits, sets, bolts, machines and tests piping systems for facilities that cannot fail. Every joint runs through NODARC Nexus, our own quality system, so the record is complete the day the system is.
Each market fails in its own way: an outage, a particle, an audit finding, a leak, a breach of base rules. We plan the work around the failure the owner fears most.
Chilled and condenser water, cooling loops and CDU connections, generator fuel. Tie-ins beside live systems under owner-approved methods of procedure, with foreign-material control and commissioning-ready records.
The failure: an outageStainless process and utility piping, bulk gas, process cooling water and clean dry air, built with purge control, contamination discipline and coupon records under the owner's cleanroom protocol.
The failure: a particlePurified water, WFI, clean steam and CIP stainless, with weld logs, borescope records and good documentation practice that support the owner's validation.
The failure: an audit findingRefining, chemical, ammonia and LNG piping, tie-ins and equipment, including turnarounds and outages, with PWHT, PMI and controlled bolting.
The failure: a leakCentral plant, hangar, utility and fuel piping on Air Force installations, with an accident prevention plan, activity hazard analyses, base-access discipline and complete submittals.
The failure: a breach of base rulesMost contractors assemble the turnover book at the end. We build it as we weld. Nexus links every weld and flange joint to its drawing, material, procedure, welder, inspection, NDE and test, so nothing is reconstructed later.
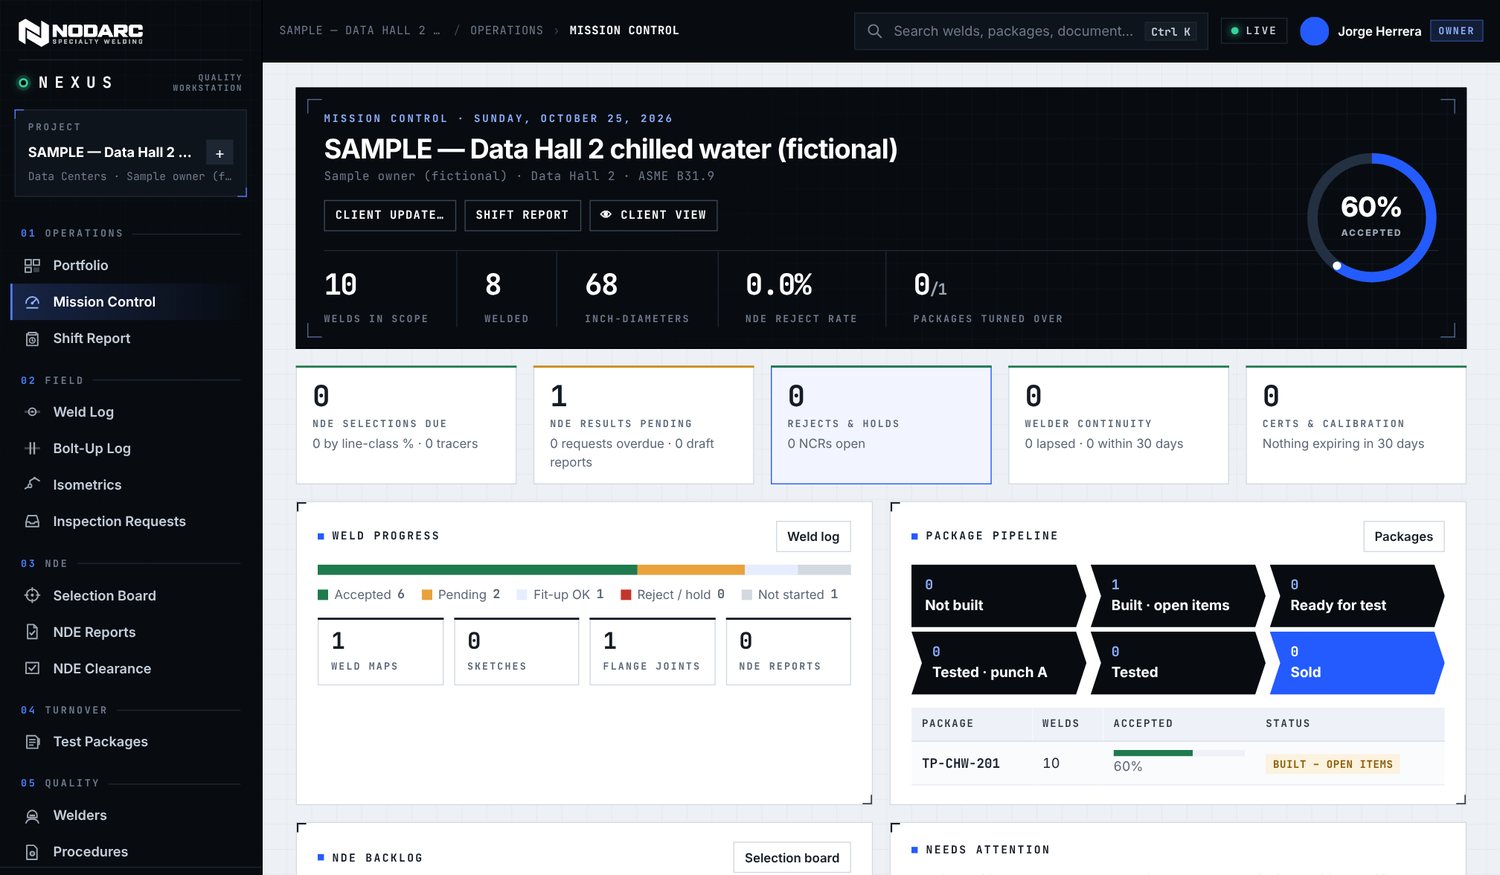
The whole job on one screen: welds, NDE backlog, package pipeline, welder continuity and expiring certificates.
Every test package follows the same path. Each step has an owner, a record and a signature, and the next step waits until the last is closed.
Once you accept a package, QC issues numbered field copies to the people doing the work. Each is logged to its holder, and a new revision voids the old one.
The full inspection package for the field inspector, with hold points and a field-change log.
What the crew needs at the work and nothing it doesn't, with a stop-and-call-QC page.
Every tab from cover to correspondence, with contents, dividers and digital signatures.
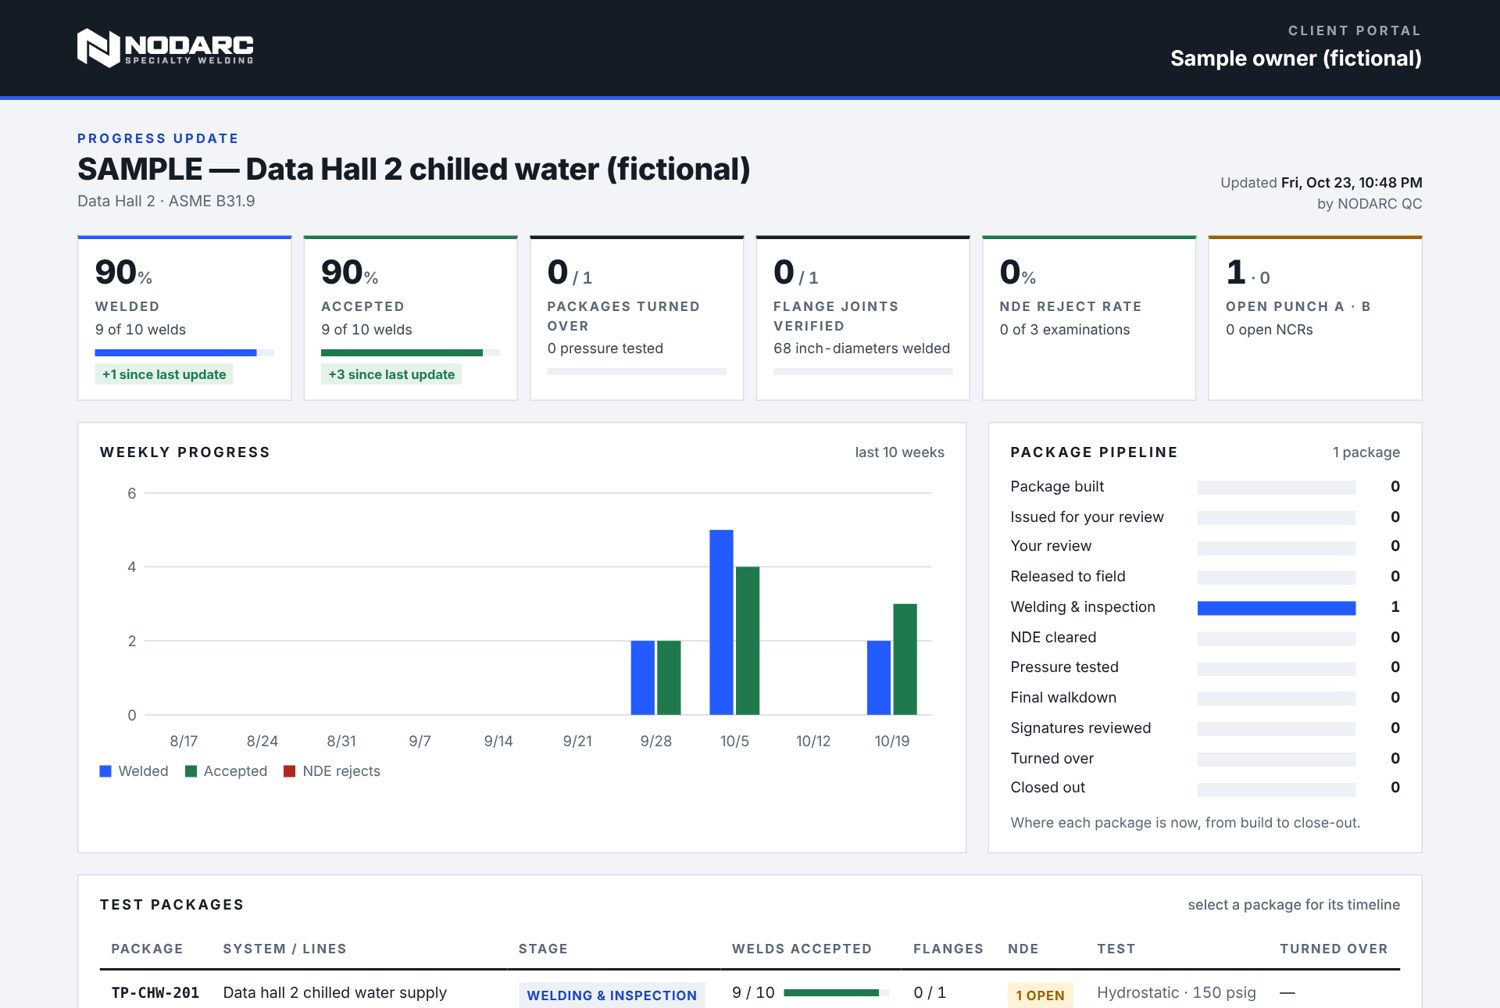
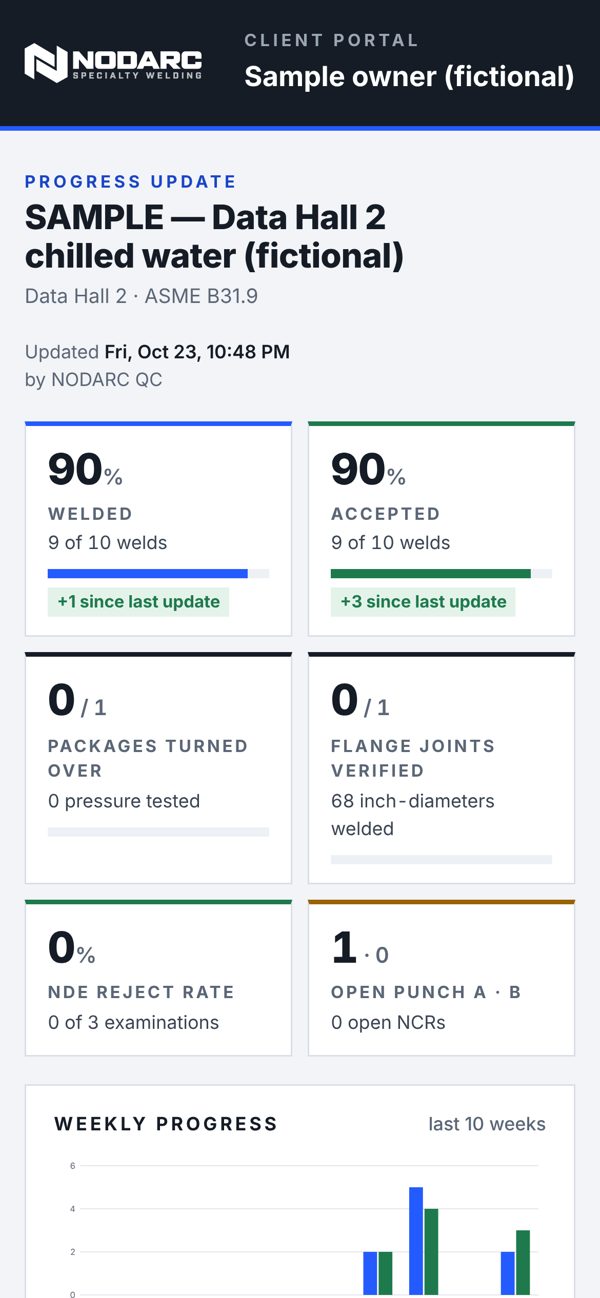
Every client gets a private portal that shows their project and nothing else. Open it from a QR code on your phone or at your desk.
Every proposal names the lines included and exactly where our scope begins and ends.
Carbon and stainless pipe, shop and field. GTAW roots, GTAW/SMAW combinations, tie-ins and repairs.
Spools, manifolds and supports fitted to isometrics, with heat numbers carried onto every piece.
Setting, leveling, aligning and connecting pumps, skids, exchangers and packaged units.
Field installation and tie-ins, hydrostatic and pneumatic testing to approved test packages.
Controlled bolting with calibrated hydraulic tools, sequenced passes and tagged joints to ASME PCC-1.
Flange facing, cold cutting and beveling, baseplate and coupling alignment with recorded readings.
Look-ahead schedules, written change control and a weekly progress and quality report.
Weld maps, weld and flange logs, NDE coordination and indexed turnover packages by system.
Not in our scope: design and engineering, structural steel erection, electrical work and alkylation-unit services. When a project needs them, the proposal names who provides them.
Quality is led by AWS Certified Welding Inspectors, independent of production. Our own project record starts with our first job, and we are glad to begin with a scope sized to our current capacity.
| Welding process | Application | Status |
|---|---|---|
| GTAW / SMAW | P1 carbon steel pipe, all positions | In qualification |
| GTAW | P8 stainless pipe with argon back purge | In qualification |
| SMAW | Uphill E6010 / E7018; downhill E8010-P1 | In qualification |
| Orbital GTAW | 316L high-purity and ASME BPE hygienic tube | Planned |
| Nexus | Quality system, field copies and client portal | In use |
We respond with a written proposal that states exactly what is included and excluded, the schedule basis and our time-and-material rates. To quote accurately, send:
Ask for our capability statement, quality manual, safety programs or prequalification package.